The short answer
An AQL inspection plan should identify the lot, sampling standard and edition, inspection level, AQL values by defect class, sampling route and acceptance/rejection rule. It must also define product-specific defects and compare units with the approved sample, measurements, BOM, color, branding and packaging requirements.
Do not translate AQL into “percent defects allowed.”
Define critical, major and minor examples before inspection.
Keep laboratory tests and final visual inspection as separate evidence.
Name the sampling system completely
ISO 2859-1:2026 defines AQL-indexed sampling schemes for lot-by-lot inspection. State the lot definition, level, plan and edition. The resulting sample size and acceptance numbers come from that system, not from multiplying the lot by the AQL number.
Build the defect library for yoga wear
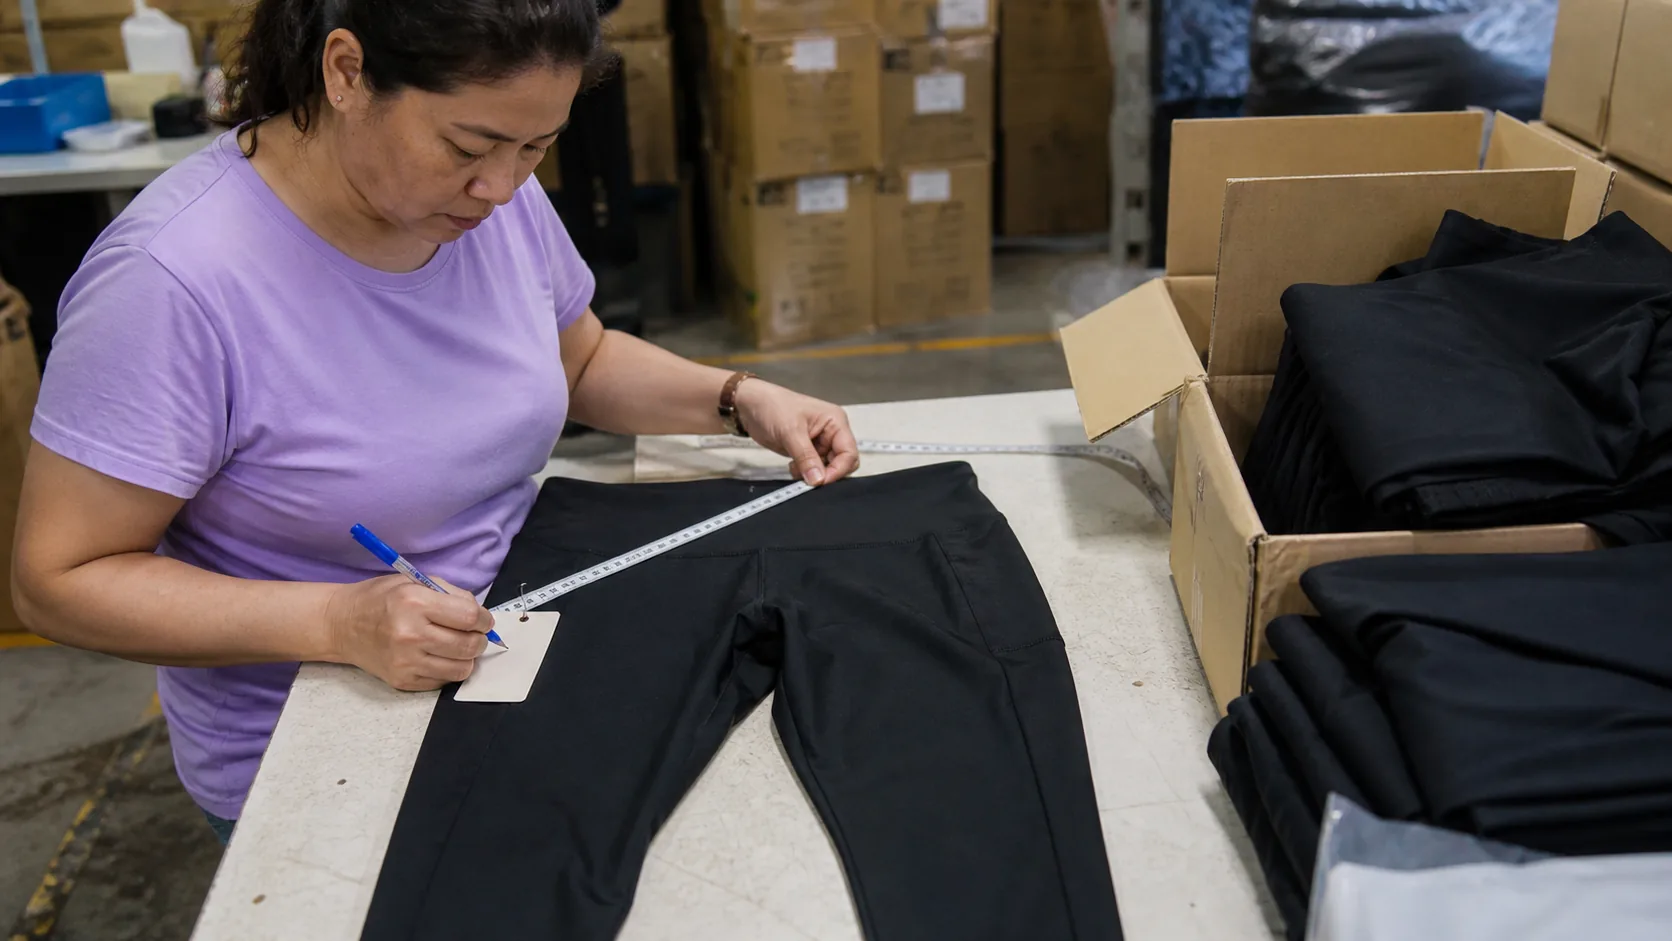
Examples can include wrong product identity, unsafe components, open seams, skipped stitches, measurement failures, asymmetric panels, shade mismatch, visible contamination, branding errors and packing mistakes. Classify each example based on actual customer and compliance risk.
Add product-specific checks
Final inspection can verify workmanship and agreed simple functions, such as pocket retention or elastic presence, but it does not replace laboratory testing or a full fit program. Name which checks are visual, measured, functional or document review.
Define hold and release decisions
Write who receives the report, who can approve rework or deviation and what requires reinspection. A pass should identify the inspected lot and reference; it should not become a blanket claim about every future order.
Decision map from this guide
| Decision area | What this guide establishes |
|---|---|
| Name the sampling system completely | ISO 2859-1:2026 defines AQL-indexed sampling schemes for lot-by-lot inspection. |
| Build the defect library for yoga wear | Examples can include wrong product identity, unsafe components, open seams, skipped stitches, measurement failures, asymmetric panels, shade mismatch, visible contamination, branding errors and packing mistakes. |
| Add product-specific checks | Final inspection can verify workmanship and agreed simple functions, such as pocket retention or elastic presence, but it does not replace laboratory testing or a full fit program. |
| Define hold and release decisions | Write who receives the report, who can approve rework or deviation and what requires reinspection. |
Sources and scope
This guide translates primary standards and public technical sources into a buyer-side development workflow. It does not replace legal advice, a purchased standard, laboratory instructions or project-specific engineering.
Buyer questions
Does AQL 2.5 mean 2.5% defective goods are accepted?
No. AQL is an index used with a defined sampling plan and acceptance/rejection numbers.
Can final inspection prove colorfastness?
No. It can review documents and visible condition, while colorfastness needs the relevant material test method and scope.
How do you read an AQL table and choose the inspection level?
Read the table in a fixed order. NIST’s engineering statistics handbook summarizes the steps of the military sampling standard from which ANSI Z1.4 and ISO 2859 descend: decide the AQL, decide the inspection level, determine the lot size, look up the sample-size code letter, choose single, double or multiple sampling, read the plan from the matching table, then start with normal inspection and follow the switching rules. An online AQL calculator or chart performs the same lookups, so check which standard and edition it copies before trusting its output.
The inspection level controls how the sample grows with the lot. NIST notes that the standard offers three general and four special levels. A level is not a quality grade: it changes how many garments are drawn from a lot of a given size, and therefore how much evidence the decision rests on. Write the level into the purchase order instead of relying on an inspector’s default, and ask for the lot size, code letter, sample size and acceptance and rejection numbers to appear in the report.
Choose the AQL separately for each defect class; the acceptance and rejection numbers then come from the table for that sample size. No formula turns a lot quantity into an allowed number of defects, and every plan carries an operating characteristic curve describing how likely it is to accept lots of different quality. Keep critical defects outside that logic with a written rule, such as holding the lot whenever one is found.
Check the edition as well. BSI’s summary of ISO 2859-1:2026 says the new edition formalizes skip-lot sampling and replaces printed operating-characteristic tables with methods for generating the curves. If a supplier manual still cites an older ISO edition or ANSI Z1.4, state in the order which document governs, so buyer, factory and inspector read the same table.
What does a third-party inspection company check, and when?
A third-party inspector is an independent firm the buyer appoints to check goods against the order, usually at the factory. Buyers use one when they cannot be present, when a customer asks for independent evidence or when they want a check the supplier does not control. Depending on the instruction, the check can take place at the factory, during container loading or after arrival. The inspector judges only what the instruction asks, so the instruction matters more than the name on the report.
| Check | Typical timing | What it can catch | What it cannot prove |
|---|---|---|---|
| Pre-production check | Before cutting starts | Wrong fabric, trims or colors, or missing approvals | How consistently the line will sew |
| During-production check | Early in sewing | Repeating workmanship or measurement faults while correction is cheap | The finished and packed condition |
| Final random inspection | Goods finished and mostly packed | Workmanship, measurements, labels and packing on a random sample under the agreed plan | Laboratory properties such as colorfastness or shrinkage |
| Loading check | At container loading | Carton count, carton marks and loading condition | The quality of garments in unopened cartons |
Send the inspector the approved sample or reference photos, the current specification, a defect list with classes, the sampling plan and packing instructions. Agree in advance who pays for re-inspection after a failure and who decides on rework or release. For a first order, a during-production check can catch a repeating fault before the whole lot is sewn. Treat the report as evidence about one lot on one date, not as a quality certificate for later orders; the production and quality planning route shows how the inspection instruction fits the release packet.
More buyer questions
What does AQL stand for?
In ISO 2859-1, AQL stands for acceptance quality limit; other texts, including NIST’s engineering statistics handbook, expand it as acceptable quality level. Both name the quality index a sampling plan is built around, not a share of defective garments you agree to receive. Quote the standard and edition with the value so everyone uses the same table.
What AQL level should I use?
Choose values per defect class from product risk and write them into the order. Set a stricter value for major defects than for minor ones, and handle critical defects with a separate rule. Base the choice on price point, customer expectations, previous inspection results and how costly a defect is to fix after delivery; no single value suits every product.
How do AQL, LTPD and AOQL differ?
AQL and LTPD mark two ends of one plan, while AOQL describes an outcome. NIST explains the AQL as baseline quality the plan should accept with high probability, the LTPD as poor quality it should accept only with very low probability, and the AOQL as the worst long-run average outgoing quality when rejected lots are fully screened. Minitab’s acceptance-sampling documentation calls the LTPD point the rejectable quality level (RQL).
What is a third-party inspection report or certificate?
It is the inspector’s record of one lot: order and style references, sampling plan and quantities, defects found by class, measurements, packing and labeling checks, photos and a pass, fail or pending result. A summary certificate may be issued, but either document covers only that lot, that date and the instruction given, not the factory’s future production.
How much does third-party inspection cost?
There is no universal price. Quotes depend on location, product, sample size, inspection type, travel and reporting, so ask whether the price is per inspector-day or per visit and what a re-inspection after a failure costs. Compare firms on the same sampling plan and checklist, because a cheaper quote may simply inspect less.
Which third-party inspection companies operate in China?
Many do, from large international testing and inspection groups to smaller local firms, and no neutral ranking picks the best one. Choose by fit rather than name: confirm that the firm covers the factory’s city, performs the checks you need, shares inspector qualifications and a sample report, and follows your written instruction instead of a generic checklist.
Additional sources
- NIST/SEMATECH e-Handbook of Statistical Methods: AQL, LTPD, AOQL and MIL Standard plans (reviewed 27 September 2026)
- BSI Knowledge: BS ISO 2859-1:2026, sampling schemes indexed by acceptance quality limit (reviewed 27 September 2026)
- Minitab Support: Attributes acceptance sampling—AQL and rejectable quality level (reviewed 27 September 2026)
